 Stocktake Preparation for a Busy Woodworking Shop
Inventory2 min read
Stocktake Preparation for a Busy Woodworking Shop
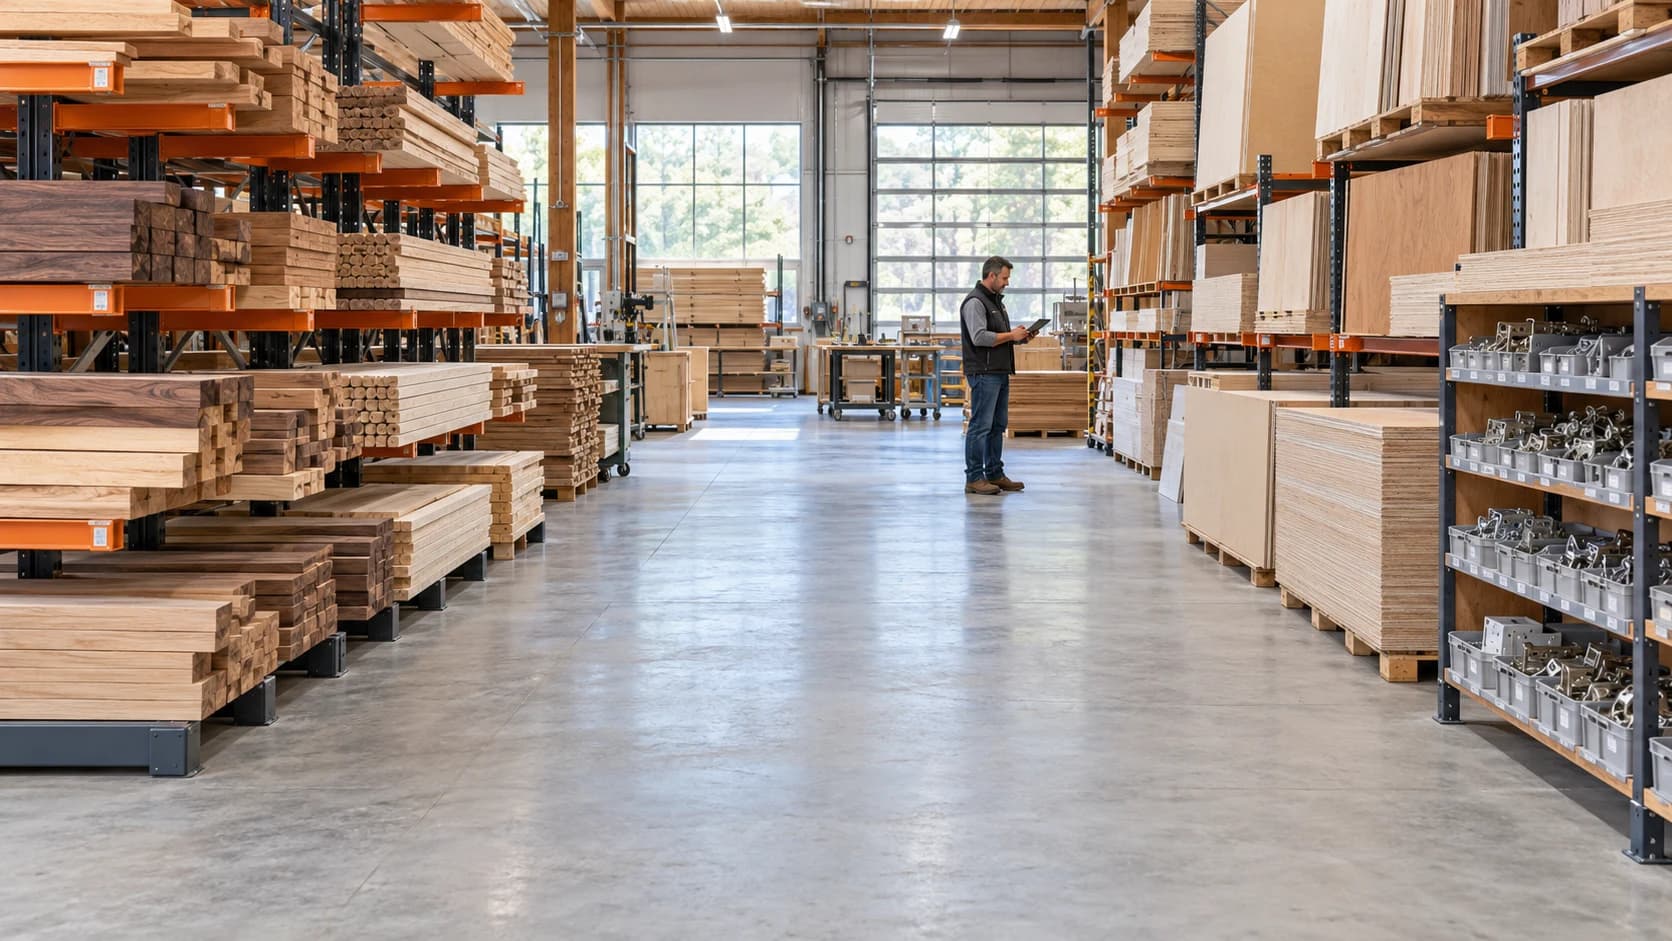
A stocktake is easier to trust when the warehouse is prepared before counting starts.
Archive ·Cycle counting checks a manageable selection of stock on a regular schedule.
Cycle Counting for a Woodworking WarehouseCycle counting checks a manageable selection of stock on a regular schedule. In a woodworking warehouse, start with hardware and sheet goods that frequently cause shortages, then expand the routine. The value comes from investigating discrepancies, not just changing the number in a system.
The system shows 48 hinge pairs and the shelf contains three boxes of 20. Before adding 12 pairs, check whether the boxes are complete and whether a recent receipt was recorded as boxes rather than pairs. Correcting the unit error prevents the same discrepancy returning next week.
Track discrepancies by cause and location, along with the number of repeated errors. A higher count frequency cannot compensate for receipts that never get recorded.
A count by item must include every location where that item can legitimately exist. A count by location must include every item inside that boundary. Either approach can work; problems arise when a team starts with one definition and finishes with the other. Mark work-in-progress, customer-owned goods, and material awaiting inspection so counters know how to treat them.
Choose a cutoff time and record movements around it. If ten pairs leave a bin while the counter is working, a later system comparison can appear wrong even when both the count and the transaction are accurate. A temporary movement pause is simple; a documented movement log is another option where a pause is impractical.
Trace the last few receipts, issues, returns, and transfers. Look for a correct transaction against the wrong item or location, as well as missing transactions. A positive variance in one bin and an equal negative variance in the next may indicate a transfer error rather than two independent stock errors.
Require a recount for discrepancies above the shop's chosen tolerance, and make that tolerance appropriate to the material. There is no universal percentage that makes a missing custom component acceptable. Record the cause, correction, reviewer, and any process change so the next count can test whether the fix worked.
An absolute quantity or value discrepancy helps prioritize investigation; recurring causes reveal process weakness. Keep both views. A count programme can show improving aggregate accuracy while one receiving step continues to generate the same unit-conversion mistake. Use the findings to improve that step instead of simply counting the affected bin more often.
Oracle overview of cycle counting. Consult the current source for its specific scope and requirements.
When a component shortage or material change affects a job, start with the recorded stock and the work it supports. Millbase inventory keeps quantities, material costs, receipts, stock lots, and usage history together. Use project tracking to review the associated labour and material costs, then reconcile the physical material before making a new commitment.
Ask the Millbase AI agent a question grounded in your workspace records. For example: “What inventory records do we have for this material, and what usage is recorded against this project?” You can select a project or worker, ask follow-up questions, and request supported reports and CSV exports.
Use the answer to locate the relevant records and investigate the exception. A physical count, approved specification, or supplier confirmation still establishes facts that have not been recorded.
Usually only the counted stock needs a controlled movement window. If stock must move, record the timing and quantities so the comparison uses the same point in time.
Prioritize items with costly shortages, frequent movements, unreliable records, or high value. Review the priorities as the evidence changes.
Writing about woodworking, millwork, and the operations behind a better-run shop.
Connect on LinkedInExplore how Millbase connects projects, people, inventory, and labor records.
Book a live demoStocktake Preparation for a Busy Woodworking ShopA stocktake is easier to trust when the warehouse is prepared before counting starts.
Archive ·A 30-Day Inventory Cleanup Plan for a Cabinet ShopA 30-day cleanup can establish a reliable starting point if the scope is realistic.
Archive ·A Weekly Inventory Review for Cabinet Shop ManagersA weekly inventory review should focus on exceptions that could interrupt released work.
Archive ·