 Customer Updates Based on Actual Cabinet Job Progress
Production2 min read
Customer Updates Based on Actual Cabinet Job Progress
A useful customer update connects progress with the agreed scope and next commitment.
Archive ·A workstation queue should contain work the station can actually process.
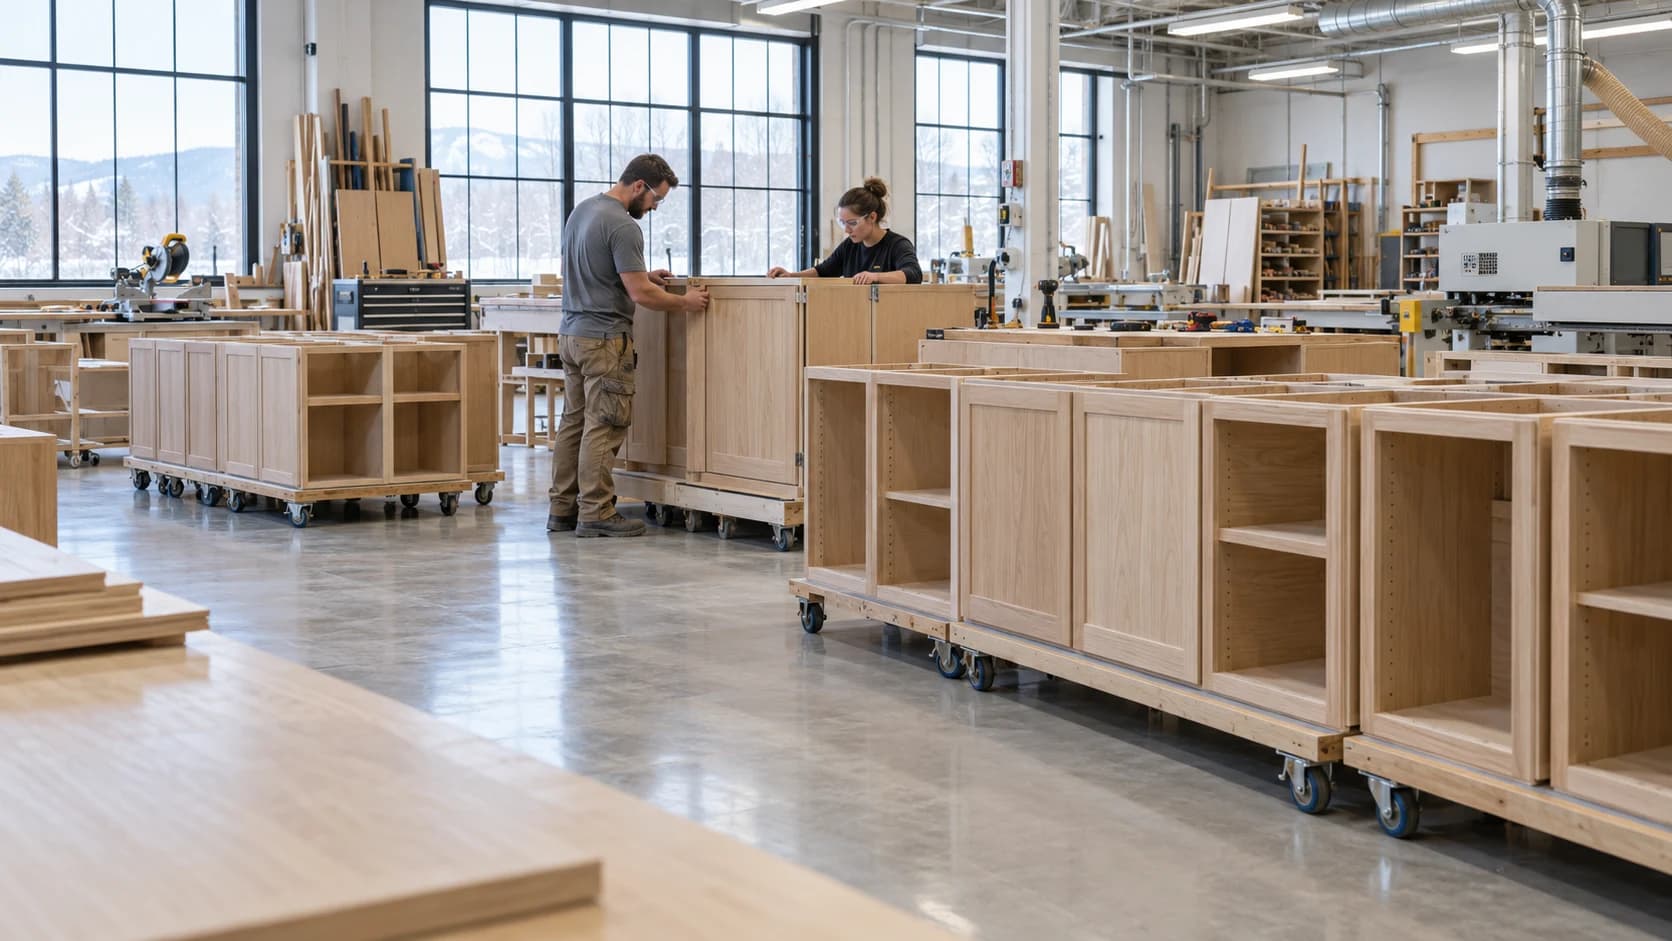
Workstation Queues: Make the Next Job ReadyA workstation queue should contain work the station can actually process. Mixing ready kits with jobs missing drawings or hardware makes the queue look larger than usable work. Separate readiness from priority so operators do not repeatedly discover the same blockers.
A hypothetical assembly area has six carts, but only two contain complete kits. Reporting six jobs ready overstates the available work. Label the four exceptions and resolve their missing inputs rather than asking the operator to choose among incomplete carts.
Track how long ready work waits and how long blocked work remains unresolved. These measures point to different interventions.
A woodworking schedule is easier to review when the team can see the work already recorded. Millbase Floor Pulse shows active workers, projects, workstations, and elapsed time. Pair it with project records to discuss a delayed cabinet order with the people and work behind it, and compare logged labour with the estimate.
Ask the Millbase AI agent a question grounded in your workspace records. For example: “Who is working on this project, at which workstations, and how many hours have been recorded?” You can select a project or worker, ask follow-up questions, and request supported reports and CSV exports.
Use the breakdown to prepare the next production conversation. Current activity and recorded hours are evidence for planning; they do not by themselves prove that an assembly has passed inspection or is ready to ship.
For the broader workflow and decisions behind this guide, read Production Scheduling for Custom Cabinetry.
Give them clear priorities and an escalation path. Local discretion can help, but it should not silently override customer or downstream commitments.
Sometimes a small buffer helps, but excessive queues consume space and hide problems. Evaluate usable output and delivery.
Writing about woodworking, millwork, and the operations behind a better-run shop.
Connect on LinkedInExplore how Millbase connects projects, people, inventory, and labor records.
Book a live demoCustomer Updates Based on Actual Cabinet Job ProgressA useful customer update connects progress with the agreed scope and next commitment.
Archive ·Managing Planned Maintenance in a Cabinet Production SchedulePlanned maintenance consumes capacity and should be visible before jobs are promised.
Archive ·Shift Handoffs in a Woodworking FactoryA shift handoff should preserve the state of work, open problems, and the next safe authorized action.
Archive ·